Don’t go!
Please get in touch, and our engineers will draw up a bespoke solution for your project.

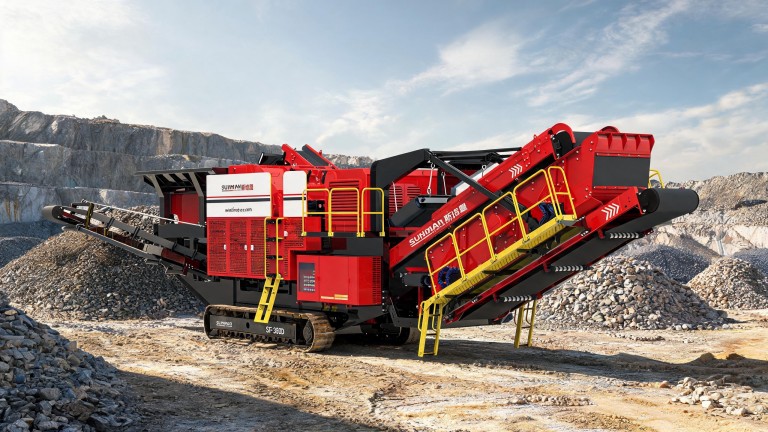
It is possible to crush river stone using a mobile rotary crusher without excessive wear, provided that the specified operating conditions are adhered to; this has been confirmed by tests, and the influencing factors are outlined, along with a comparison with other raw materials.

Before feeding the crushers, the permissible clay content in limestone is up to 8% (for rotary crushers, 1% lower), and temporarily up to 10% provided the moisture content is ≤2%. Exceeding this limit reduces throughput and increases the risk of blockages; this is controlled by flushing the fraction.

The mobile crusher operates reliably with damp clay up to 22% without any modifications; with modifications (vibrating screens, etc.), moisture content of up to 29% is permissible; above 30%, the continuous operating time is less than 40 minutes.

If the quartz content is ≥18%, it is advisable to replace the rotary crusher with a cone crusher: the rotary crusher is designed for quartz <18%, hardness up to 6 on the Mohs scale; at 20% quartz, its wear rate is 3.2 times higher; the conical one can withstand up to 45% quartz.

A rotary crusher is cost-effective for rocks with a Mohs hardness of up to 7 units, ideally 2–6 units. Above 7 units, component wear and costs rise sharply, efficiency falls, and processing above this threshold is only feasible in the short term.

A single rotary crusher can process both limestone and granite, provided the following parameters are observed: rotor speed 38–45 m/s, hammers ≥62 HRC, piece sizes of 500 and 350 mm, and replacement of hammers when worn down to 30%.

A single mobile line can produce four fractions simultaneously; throughput falls by 12–18%; three screens and four conveyors are required; maintenance is required more frequently by 10%; fractions are changed simply by replacing the screens.

It is possible to obtain a 5–10 mm product fraction without a second stage of crushing, provided that the requirements for the raw material and the settings for the crusher and screen are met; the proportion of the target fraction reaches 78%.

The mobile rotary crusher produces 86% of cuboidal aggregate when processing granite; this figure, which depends on the feed material, rotor speed and wear on components, is higher than that achieved by jaw and cone crushers.

When the gap in the jaw crusher is reduced by 10 mm, the proportion of fine (by 19–28 percentage points) and dust-like (by 4–6 percentage points) fractions increases, the proportion of coarse particles decreases (by 35–42 percentage points), and the uniformity improves; these parameters depend on the initial gap and the material.