Artificial Sand Crusher Price: Key Cost Factors and Budget Guide
Find out what factors determine the price of an artificial sand crusher (VSI): feed size, rock hardness, capacity, wear parts and total plant costs. Essential budgeting
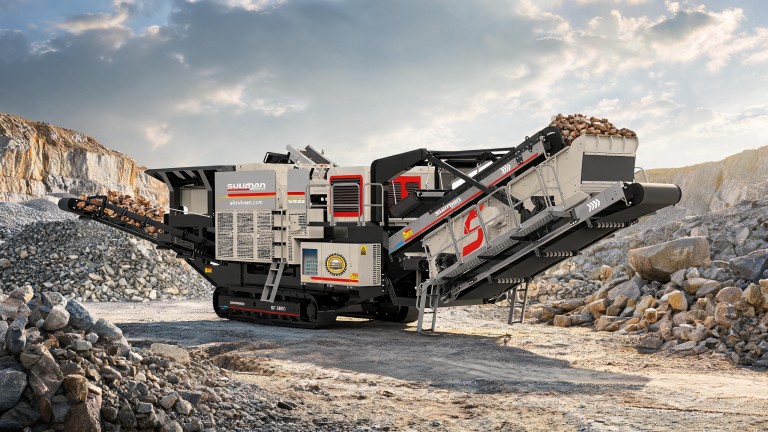
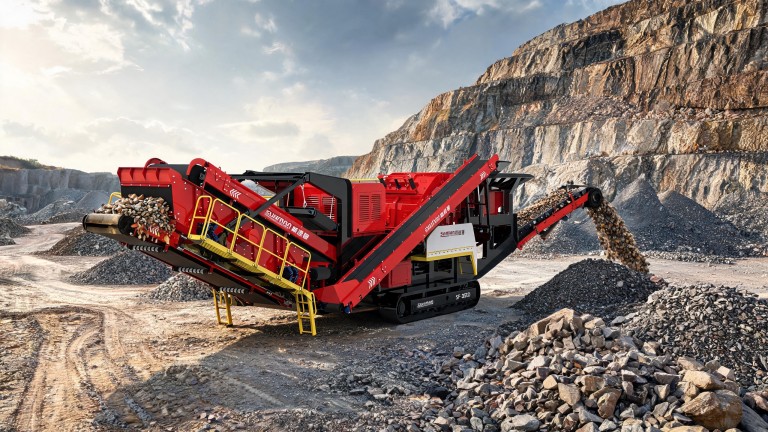
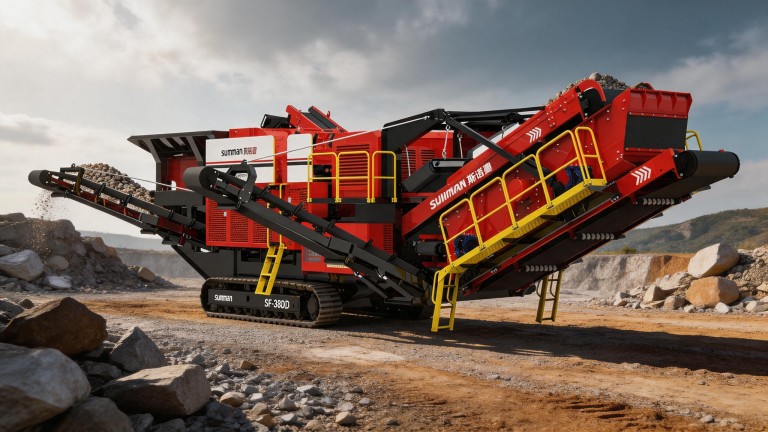
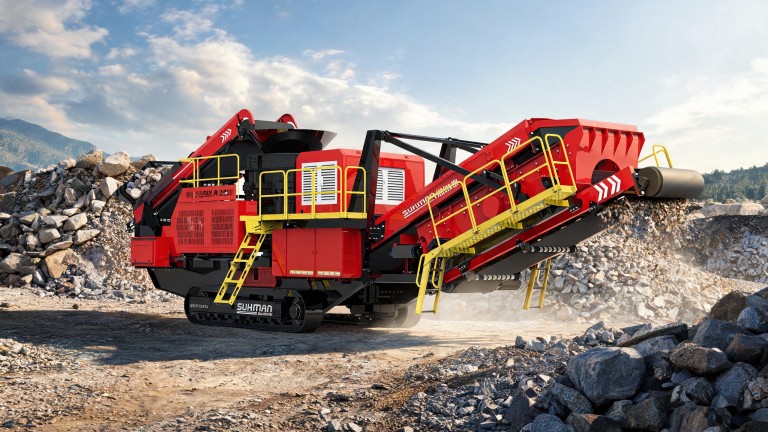
The price of an artificial sand crusher (máy nghiền cát nhân tạo) cannot be quoted as a single figure because the equipment is configured to suit the source rock, feed size, target capacity and final sand specification. In practical terms, a quarry owner in Vietnam should expect the quote to be based on a vertical shaft impact (VSI) crusher as the core unit, with the final price varying according to rotor diameter, motor power, level of automation and downstream screening. As no verified SUHMAN price list is available in this article, any figure below that is marked as an approximate estimate must be confirmed with the manufacturer or your local dealer before finalising your budget.
What actually determines the price
The purchase price is merely the entry threshold. For a quarry producing construction sand, the total cost comprises the feed system, the crusher itself, the vibrating screen (closed or open circuit), chutes and conveyors, foundation works, and the electrical control panel. At many Vietnamese quarry sites, the crusher body accounts for roughly half the total cost of the sand-making plant, but this proportion varies depending on the hardness of the feed rock. A feed of granite or basalt requires more wear-resistant parts and a heavier rotor, which increases the base price of the machine.
Feed conditions are more important than most buyers realise. A VSI crusher is designed for clean, dry feed between approximately 5 mm and 50 mm. If your quarry feed contains high levels of moisture or clay contamination, you will need additional feeding and screening equipment, and the downstream sand may need to be washed — both of these represent separate cost items. For typical river pebbles, limestone or granite, the VSI configuration is tried and tested, but the wear cost per tonne of sand produced varies significantly depending on the abrasiveness of the rock.
Checklist of things to consider before requesting a quote
Please use the table below as a structured list of requirements. Fill in each row with your actual site data; without this information, any price estimate will be mere guesswork.
Parameter you must provide
What to specify
Why it affects the price
Status
Target capacity
Tonnes per hour of finished sand (e.g., 50, 100, 200 t/h)
Higher throughput means a larger rotor, motor and chassis
To be confirmed
Feed material
Rock type, hardness (Mohs), silica content, moisture %
A high silica content increases wear costs and may require a thicker rotor feed tube
To be confirmed
Feed size distribution
Maximum feed size (mm) and typical particle shape
Oversized feed requires a pre-crusher or grizzly screen, which increases costs
To be confirmed
Final sand specification
Fineness modulus, apparent density, maximum dust content
Controls for screening and dedusting/washing options
To be confirmed
Process mode
Dry or wet production
The wet process involves additional costs for washing equipment and water management
To be confirmed
On-site power supply
Voltage, available kVA, grid stability
Motor size and soft-start or VFD options depend on the power supply at the site
To be confirmed
Installation site
Ground level, area, ground conditions
Anchoring, concrete works and lifting equipment affect installation costs
To be confirmed
Engineering estimates versus measured facts
When you receive a quotation, distinguish between the measured data and the manufacturer’s estimates. The crusher throughput and rotor tip speed can be calculated from the machine’s operating curve, and these are engineering estimates that should be included in the technical data sheet. The final sand gradation, however, can only be confirmed by a field test — either a pilot test using your own rock or a reference project where the same rock type was processed. Many suppliers quote a «nominal» output for soft limestone, but your granite quarry will yield a lower output per machine hour. Ask for the output figure specified for a particular feed size, moisture content and closed-side setting; if the supplier provides a single figure without these conditions, treat it as indicative only.
Running costs that exceed the purchase price
For a quarry manager, the total cost of ownership over five years usually exceeds the initial purchase price. In VSI crushers, the wear parts — the rotor tip, wear plates and the anvil ring or rock shelf — represent the largest recurring expense. With abrasive materials such as granite with a high quartz content, wear consumables can become the dominant cost, so the hardness and thickness of these parts directly affect your production cost per tonne. Power consumption is the second major cost; motor efficiency and idle-running control can be assessed based on the installed motor power and electrical draw per tonne. Neither of these figures can be confirmed without either the manufacturer’s test records or a reference installation on similar rock.
Suitability boundary — when a VSI sand machine is the right choice
A VSI crusher is suitable when your quarry produces 30–300 t/h of manufactured sand from dry, hard, blocky feed, and when the final sand requires a cubic shape and a tight gradation for concrete or asphalt. The machine excels at rock-on-rock crushing, where operating costs are minimised by using the material itself as the crushing medium. This means you should choose a VSI when the feed size is already under 50 mm and the target product is fine aggregates.
Where the recommendation does not apply
The VSI approach is not suitable when the feed contains sticky clay, has a high moisture content (above roughly 8%), or consists of materials that adhere to the rotor walls. In such cases, washing and screening become necessary prior to the VSI, and the system becomes more expensive and labour-intensive to maintain than an alternative such as a selective impact crusher or a tertiary cone crusher with a screen. Furthermore, if the source rock is extremely abrasive — for example, high-silica quartzite — the wear cost per tonne of sand may render the VSI economically unviable, and a different crushing approach should be considered.
Missing information that you must provide for the final selection
Before any supplier can provide you with a firm price, you must provide the following in your official site documentation: a representative rock sample weighing 200–500 kg for testing, the intended production capacity in tonnes per hour of finished sand, the permitted dust content in the final product, and the available power supply at the site. You also need to specify the concrete standard to which your product must conform (e.g., TCVN 7570 in Vietnam), as this determines the fineness and grading of the sand that you must meet. Without this information, a supplier’s quotation is merely a guide, not a firm commitment.
FAQ — Frequently Asked Questions
What is the difference between a VSI and a cone crusher when it comes to sand production?
A cone crusher compresses rock between an eccentrically rotating mantle and a concave liner, producing more fines but with a less cubic shape. A VSI (vertical shaft impact) crusher accelerates rock against a rock bed or anvil, resulting in a better particle shape in the fine fraction and a tighter distribution of sand sizes. For manufactured sand, the VSI is usually the final shaping stage, whilst the cone crusher operates at the secondary or tertiary stage to reduce particle size prior to the VSI. The price difference between the two is substantial and depends on the feed size and throughput targets; therefore, a comparison should only be made once your material tests have been completed.
Does a high moisture content in the feed affect the price of the sand crusher?
Yes. A VSI crusher does not handle sticky, wet feed material well; moisture content above 6–8% can cause build-up in the rotor and reduce effective throughput. To ensure reliable operation, you would need a drying or pre-screening system, and for wet-only processes, sand washing equipment should be installed downstream of the crusher. Both of these additions increase the initial cost and the running costs. If your quarry experiences seasonal rainfall, as is common in southern Vietnam, the procurement decision should take into account a wet-season plan, not just a dry-season trial.
What operating costs should I budget for in terms of parts and energy?
The purchase price is a one-off cost, but wear parts and electricity are ongoing expenses. Wear part consumption is proportional to the abrasiveness of the feed; the service life of the rotor tips can vary by a factor of several times between soft limestone and hard granite. Energy costs are roughly proportional to the motor power and the operating hours, but the actual consumption per tonne can only be measured on site. Ask the supplier for a documented wear-life figure for a similar rock type and a measured or verified specific energy figure; if neither is available, this must be noted in the quotation.
Should I buy a complete sand-making plant or a single crusher?
If you already have an aggregate crushing line producing 5–50 mm feed, purchasing a stand-alone VSI crusher and a screening module may be sufficient. If you are starting from a quarry face, you will need the full sequence: feeder, primary jaw or impact crusher, secondary crusher, VSI, screen, and possibly a sand washer. The price of the complete plant is a multiple of the price of a single crusher, and the key factors needed to make that decision are the total project capacity, the land area, and the mix of end products you plan to sell.
How long does a VSI rotor last, and how does that affect the quote?
The rotor is the component subject to the greatest load. Its service life is determined by the material of the wear parts and the rotor tip speed, which is dictated by the hardness of the feed material. There is no one-size-fits-all answer: for the same rock type, a low tip speed results in a long rotor life but a limited specific output, whereas a higher speed produces more fines but causes the rotor to wear out more quickly. Your supplier should provide the rotor’s service life in hours at the configured tip speed for your specific rock type — if the quotation merely describes the rotor as «wear-resistant» without specifying hours, ask for clarification before comparing prices.